


[ad_1]
We get requested a variety of questions on 3D printing, and rightfully so; it’s an advanced world! After spending numerous hours answering cellphone calls and emails, we realized we should always most likely have a useful resource for some primary data, to assist these new to the wonderful 3D printing universe. So with out additional ado, welcome to the…
You may have some questions, we now have some solutions.
1. How a lot stuff can I print with one roll of filament?
A: With a view to reply this, we have to take into account just a few issues. I’m gonna throw out some jargon, however don’t fear, I’ll clarify all of it in a minute.
• We have to know the size of the article
• We have to know the share of infill
• We have to know whether or not or not the half requires assist materials
For starters, we all know that every roll of filament is 1 kg, or round 2.2 lbs of fabric. So with the intention to decide how a lot we are able to get out of this, we want a pattern half. We’ll start with one thing easy, like a chess piece. We’ll use a pawn for this instance.
So the very first thing that I do after I need to decide the burden of a component, is open up the software program MatterControl. (It’s a printer management software program accessible totally free on our web site.) Then I drag the file for the half I want to take a look at, and drop it in the primary window. From there:
1. I click on “Superior Controls”
2. I click on Slice Settings
3. I am going to the “infill” menu choice
4. I set the worth to “.5”
Observe that you may set the worth wherever between 0 and 1. Infill is the plastic contained in the half that gives inner assist. You may have the choice of constructing it fully hole, or making it fully strong. For testing functions, we’re going to place it at a hefty 50 p.c.
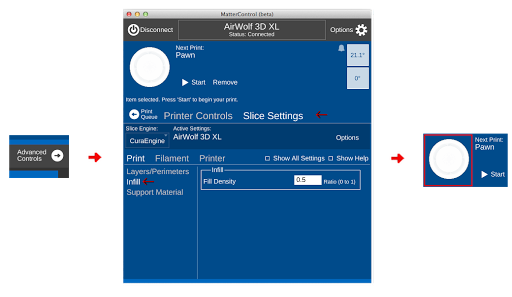
Observe the arrows!
Now:
1. Save your modifications
2. Click on on the preview window for the half you’ve gotten chosen.
3. Swap from 3D view to layer view
4. Press generate.
The window will now slice the half. As soon as it finishes, it will provide you with details about how a lot it weighs, how a lot plastic shall be extruded, and a tough estimate of how lengthy it’ll take. As soon as you recognize the burden of your half, you may decide how a lot materials shall be used. Merely divide the whole weight of the filament roll, by the burden of the half you want to create, and you’ve got an in depth estimate of what number of you may make. Within the case of this small chess piece, at a 50 p.c infill, the quantity is 121.3.
Wow, that’s a variety of chess items!
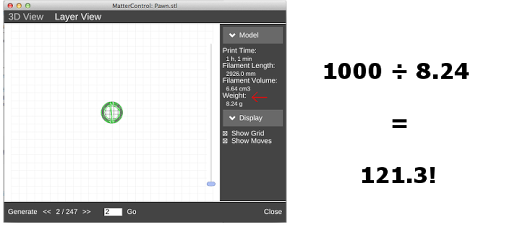
Aww, no person advised me I needed to do math!
If you wish to make one thing greater after all, the method is strictly the identical. That’s except you print one thing requiring…
SUPPORT MATERIAL
Help materials is just like infill besides it used on the surface of an object. Sometimes it’s used when an object has an overhang or bridge. Sizzling plastic doesn’t droop itself within the air very properly, so on giant or sophisticated components, it might be sensible to allow assist materials. Help materials is a little bit of sport changer although, as a result of it does require further filament. Simply you’ll want to take discover of whether or not or not assist materials is enabled earlier than you establish the whole weight.
2. How lengthy will my print take to complete?
A: I briefly talked about above how when slicing an object to seek out out it’s properties, additionally, you will see a time estimate. Whereas that is pretty self explanatory, there are just a few layers to this that we should always take into account. With out slicing the article, you may get a primary sense of how lengthy a print will take by understanding some key slicing choices. These are:
1. Layer Top
2. Infill
3. Print Pace
4. Help Materials
1. Layer Top is a reasonably easy idea. It’s precisely the peak of every extruded layer. That is the largest issue when figuring out the print pace, as a result of quantity of layers modifications drastically, relying on the enter worth to your layer peak. You’ll find this within the slice settings as soon as once more. It must be famous that you simply can not enter a layer peak that’s bigger than the dimensions of your nozzle, and nonetheless have the layers join. Usually talking, a layer peak of .2 mm will take half the print time of a print with a layer peak of .1 mm. In case your nozzle head is .5 mm, you’ve gotten many choices for the standard, and the pace of your print.
2. We already lined the fundamentals of infill, nevertheless it’s good to recollect: in the event you enhance the infill, the quantity of plastic used goes up, and so does the print time.
3. Print Pace is a extra in-depth perform of our software program, and most printers include default settings which are suited to their use. Nevertheless, in the event you actually need to get your components finished quick, that is the place to go.
4. Once more, we briefly touched on the fundamentals of assist materials, however relying on the mannequin, it might add a major quantity of plastic to the print.
3. Why received’t the plastic extrude correctly?
A: 3D printing is hard beast, and there are various potential the explanation why your extruder is having issues. The very first thing to do, is to just be sure you know what materials you’re utilizing, and that you’ve the correct temperature settings.
Every materials has a perfect vary of temperatures*, so we’ll go over every in flip.
PLA: 190-210°C**
ABS: 220 -240°C
NYLON: 240C-250°C
LAYWOOD: 175-250°C
LAYBRICK: 165-210°C
SOFT PLA/BENDLAY: 220-235°C
GLOW IN THE DARK PLA: 185-205°C
PVA: 170-190°C
*These temperatures are suitable with most printers, however you must at all times examine with both your producer or different 3Ders to verify your printer follows the identical pointers.
**Observe for MakerBot Replicator 2 customers: The Replicator appears to run a bit cooler than different printers, so though it might appear that it’s operating on the incorrect temperature, know that the default settings are as a rule appropriate.
Should you’re having bother with any explicit filament. I like to recommend beginning on the highest advisable temperature, and with every try, scaling your temperature again 5 levels till you attain the optimum temperature to your setting. It is also necessary to make it possible for your filament is being fed into the extruder correctly. If there’s an excessive amount of rigidity, the filament can get floor out, or worse, break.
Should you strive a variety of temperatures to no avail, and also you’re positive that your filament is being fed with minimal rigidity, you will have a jammed extruder.
4. I feel I’ll have a jam, what do I do subsequent?
A: Alright, so you believe you studied your printer has jammed. Don’t panic! There are lots of issues that may be finished. We’ve a way more in-depth article, that could possibly show you how to additional, accessible right here. It must be famous that jams may be very tough, so it by no means hurts to get as a lot data as doable. Nevertheless, in the event you simply need a primary rundown, I’ll strive that will help you out right here.
The 2 commonest sort of jams are as follows:
• The print nozzle being too near the mattress, due to this fact not permitting the filament to be launched*
• Leaving the warmth on whereas the filament sits unattended for an prolonged time frame.
*This may generally be solved with a easy leveling of the mattress. Both with the {hardware} on the printer or by way of the automated mattress calibration characteristic in MatterControl.
There are two very primary methods to unclogging your hotend.
1. Warmth your printer as much as a barely larger than regular temperature, and try to push the filament by way of. For example, if in case you have a PLA jam, we advocate heating to 220°C(245°C for ABS). That is a lot larger than is critical for regular prints, however not excessive sufficient to be harmful.
2. Warmth your printer as much as the usual temperature and push the filament a part of the best way by way of. Then, permit the filament to chill to about 80°C (135°C for ABS). After it will get to that temperature, slowly retract the filament till the drive block is evident. In one of the best case situation, you’ll pull up something that the filament bonded with whereas sizzling, thereby cleansing the hotend and drive block. I’d advocate that you simply do that occasionally anyway, as a result of buildup within the extruder can sometimes trigger jams.
5. How ought to I retailer my filament?
A: At this level in your 3D printing profession, you will have come to grasp that filament is one thing that must be taken care of, to a sure extent. You see, most varieties of filament take in moisture from the air, which may make it brittle or degrade. Within the case of one thing like nylon, it will probably produce bubbles within the print. Let’s cowl the fundamentals for every sort of filament.
PLA/ABS: After we ship these supplies, we now have them sealed in a bag with a packet of dessicant. While you recieve the package deal, it is high-quality to go away them within the luggage earlier than you utilize them. When you open the package deal, it’s completely acceptable to place the filament with dessicant in a big zipper storage bag, or one thing comparable.
LAYWOOD/LAYBRICK: The packaging for this filament exposes this filament to the open air, so that you need not fear about something out of the peculiar. Preserving it someplace dry ought to suffice.
SOFT PLA/BENDLAY: Just like the earlier filament, these supplies don’t have to be saved any manner particularly. Simply protecting them from getting instantly moist must be greater than sufficient.
NYLON: Nylon however, is EXTREMELY succeptable to absorbing moisture. Even in a reasonably dry envirionment, it will probably take in the greater than sufficient to disrupt a print in as little as 24 hours. Luckily, this filament can be dried out. For that reason, it isn’t solely essential to retailer your filament in a sealed bag with dessicant, however earlier than printing, some clients have discovered it helpful to dry it within the oven at low temperatures (200°F) for an hour or two.
GLOW IN THE DARK PLA: One other filament that have to be saved in a sealed bag. This among the many barely extra absorbant filaments, so deal with with care.
PVA: While you buy this filament, it’ll are available a sealed bag with a dessicant packet, generally two. This can be a water soluble filament, so protecting it dry is completely obligatory. If it will get moist, it’ll in a short time develop into unusable. I like to recommend protecting it within the unique packaging so long as doable. If you could put it in a zipper bag, take into account doubling down on dessicant.
Sometimes in the event you observe these pointers, you should not have an issue. There are occasional exceptions, as not all environments are the identical. It must also be famous that frequent temperature fluctuations appear to extend the possibility of constructing a filament flip brittle.
6. Why received’t my prints persist with the mattress?
A: That is depending on two components: Printing materials, and print situations.
What we’ll do right here is break down every materials, and the optimum print situations for each. (These are all assuming the mattress is correctly stage, which is VERY necessary.)
PLA: Blue Painters tape OR a heated mattress with Kapton/PET tape at 60Cº (Adhesive non-compulsory)
ABS/BENDLAY: A heated mattress at 120Cº PLUS some type of adhesive
NYLON: A heated mattress at 75Cº With some type of adhesive
TPE: Blue painters tape OR a heated mattress with Kapton/PET tape at 70Cº (Adhesive non-compulsory)
PLA PLA: Blue painters tape OR a heated mattress with Kapton/PET tape at 70Cº (Adhesive non-compulsory)
LAYWOOD/LAYBRICK: Blue painters tape
As a fast apart, listed here are essentially the most generally used adhesives for 3D printing:
• Aqua Web Hairspray (Additional Maintain)
• Glue Stick
• ABS Slurry
The ABS slurry solely works with ABS, nevertheless, the opposite adhesives are suitable with all varieties of filament.
My query isn’t answered right here, the place do I am going subsequent?
A: In case your query isn’t answered right here, you will have one thing barely extra superior happening. I like to recommend looking at our assist part. We’ve many in-depth articles, concerning software program, {hardware}, and every little thing in between. Should you nonetheless can’t discover a resolution, be happy to ship us an electronic mail, or give us a name! We’re open from 9:30am – 7pm Mon-Fri and from 10am – 4pm (PST) on Saturday, and we’ll do every little thing in our energy to help you the place we are able to.
Thanks for studying this FAQ!
– The MatterHackers Crew
[ad_2]
