


[ad_1]
The extruder is without doubt one of the most necessary parts on a 3D printer. It’s accountable for sending the right amount of filament to the new finish the place it’s melted and extruded down in skinny layers to make your half. It’s necessary to notice that the extruder is just not the identical as the new finish, although these phrases are generally conflated. The extruder is often known as the “chilly finish” as a result of the filament is “chilly” when it passes by the extruder on the best way to the new finish.
There are two primary sorts of extruders at present out there – Bowden and Direct – and there’s a lot of conflicting info on the market about each. In the event you’ve learn that “Bowden extruders can’t deal with versatile filament and so they have an excessive amount of stringing”, or “Direct extruders are sluggish and have an excessive amount of backlash” and are available away confused, we’re right here to assist. We’ll stroll you thru the fundamentals to assist perceive the variations and resolve which possibility is best for you.
Extruder Fundamentals
Earlier than we go into the variations between Bowden and Direct extruders, let’s go over the similarities. All extruders have just a few issues in widespread.
Motors
All extruders have motors. Desktop 3D printers sometimes use NEMA 17 stepper motors. “NEMA 17” simply means it has a 1.7” x 1.7” faceplate. Not all NEMA 17s are alike. They are often geared, 0.9degrees/step, 1.8 levels/step, and so forth. They’ll have totally different voltage rankings, totally different present rankings, they arrive in a wide range of lengths, and might present totally different quantities of torque. These particulars aren’t terribly necessary for now, however it’s necessary to level out that none of these specs are inherently higher or worse to be used as an extruder motor. The motor necessities wanted for correct operate of your extruder will principally rely on the particular setup of the extruder meeting and printer setup.
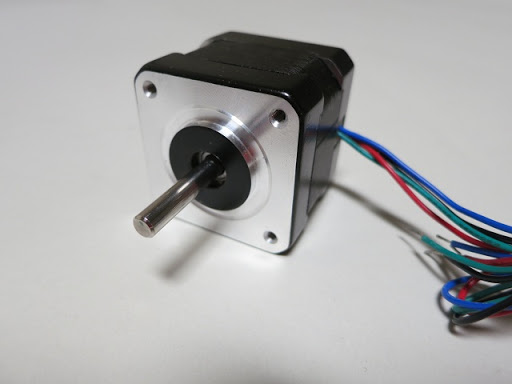
NEMA 17 Stepper Motor
Filament Drive Gear
One thing is required to ‘seize’ the filament and extrude it by the new finish. Due to the big number of extruder implementations, these usually are not all the identical. The 2 commonest ones you’ll see are small metal gears which were hobbed, and hobbed bolts. ‘Hobbed’ simply signifies that splines or tooth have been lower into it. The gears are mounted onto the motor shaft, and the bolts are sometimes pushed by geared extruder motors.
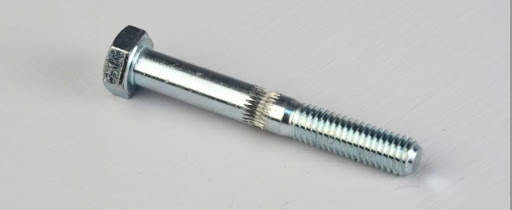
Hobbed Bolt
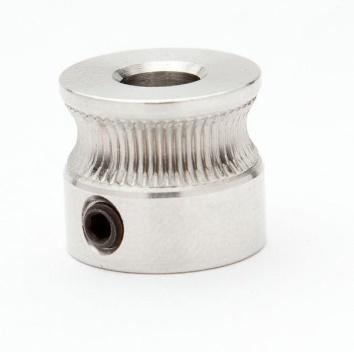
Hobbed Gear
Loafer
The loafer is the mechanism that holds the filament in opposition to the drive gear to ensure that it to be extruded by the new finish. Bearings, PTFE tubing, printed plastic, and rubber wheels have all been used. Some extruders, just like the Bondtech, use 2 drive gears. What’s necessary in regards to the loafer is that acceptable strain might be utilized in opposition to the filament on the drive gear. An excessive amount of, too little, or inconsistent strain will result in extrusion points.
Alright then, now that we’ve lined the fundamentals which might be widespread to all extruders, let’s get into the variations.
Direct Extruders
Direct extruders are merely extruders which might be straight connected to the new finish. It is a Lulzbot Mini extruder and sizzling finish. It’s a geared, direct extruder working 3mm filament.
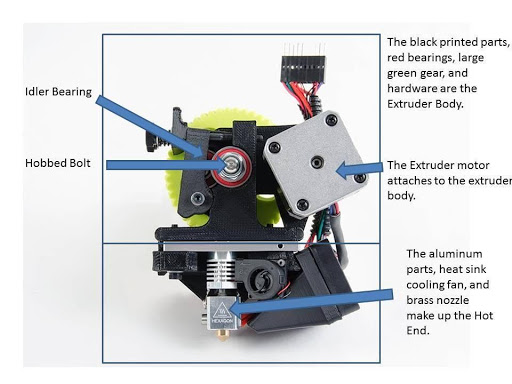
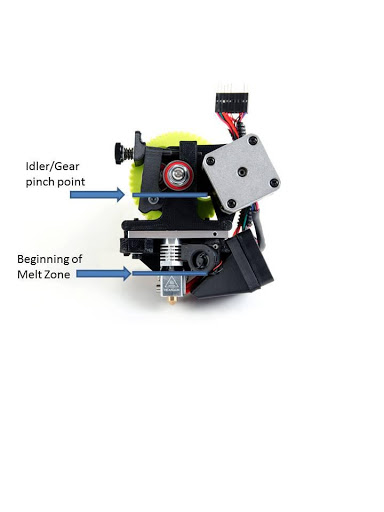
Loafer Gear and HotEnd configuration (Lulzbot)
It’s necessary to notice {that a} direct extruder is just not essentially the identical factor as a direct drive extruder. A direct drive extruder simply signifies that the filament drive mechanism is straight mounted to the motor shaft. Each bowden and direct extruders might be direct drive.
Bowden Extruders
A bowden extruder is just not straight connected to the new finish. As an alternative, a tube extends from the extruder physique to the new finish. That is referred to as a bowden tube. It’s mostly a bit of PTFE (Teflon ™ ) tubing. The filament is constrained by the tube and travels by it to the new finish. That is an EZStruder, made by SeeMeCNC. It’s a direct drive bowden extruder working 1.75mm filament.
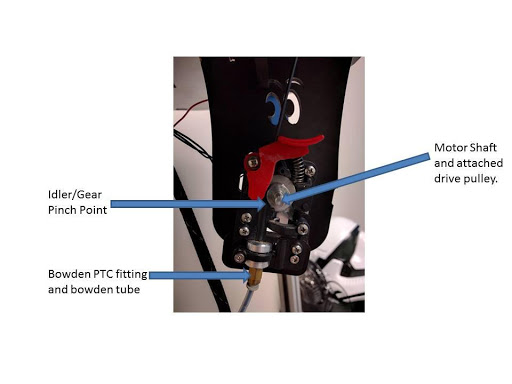
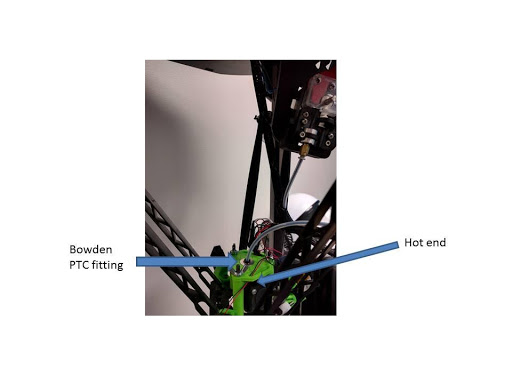
Scorching finish Aspect of Bowden Extrusion
Okay, so which is healthier?
It might be very nice if one in every of them was far superior to the opposite, however they each have their very own strengths and weaknesses.
Direct Extruder Strengths
One of many principal advantages of a direct extruder is the very brief distance between the drive mechanism (hobbed pulley or gear) and the new finish. A shorter distance provides higher responsiveness to extrusion and retractions. It additionally requires much less torque than a bowden extruder to extrude the filament by the new finish. Higher responsiveness can produce cleaner prints – this interprets to much less stringing, oozing, or different artifacts on the floor end. A decrease torque requirement means you should use a smaller motor, or you should use the identical dimension motor at a decrease present setting.
The shorter distance may also make printing with versatile supplies (like Ninjaflex, Comfortable PLA, and TPU) simpler. Although many direct extruders require slight modification to particularly deal with versatile filaments, usually, direct extruders are higher suited to flexibles than bowden extruders are.
Technical word: “Responsiveness” above is referring to the hysteresis, or lag, of the system. Direct extruders typically have much less/decrease hysteresis than bowden extruders. All different issues equal, the shorter the gap between the loafer/gear pinch level and the soften zone, the decrease the hysteresis.
Direct Extruder Weaknesses
As a result of direct extruders are straight connected to the new finish, its mass should be moved together with the new finish. Transferring extra mass round means extra chance for backlash, overshoot, and body wobble (there are different issues, however these are crucial for the needs of this text). We received’t get into technical particulars in regards to the particular mechanics concerned, however, to shortly illustrate, think about driving a automotive. It’s a lot simpler to cease in case your automotive weighs 2000lbs than if it weighs 4000lbs, proper? It’s additionally simpler to speed up and alter course, and it will get higher gasoline mileage.
The identical goes to your printer. Your printer firmware calculates acceleration, deceleration, and adjustments in course for each half. Your firmware doesn’t understand how a lot your sizzling finish carriage weighs, how stiff your printer body is, or how tight your belts are. So, in the event you don’t have good settings for acceleration and pace particular to your 3D printer, you’re more likely to expertise overshoot, backlash, body wobble (in addition to skipped or missed steps) with a direct extruder because of the elevated mass on the new finish carriage. The added mass additionally necessitates extra motor present which generates extra warmth in your motors and on the motor drivers.
Stated in another way, with all different issues being equal, you’ll be able to print sooner, extra precisely, and extra exactly with a bowden extruder than with a direct extruder as a result of you’ll be able to speed up and decelerate sooner, in addition to change instructions extra precisely and exactly as a result of much less mass on the new finish carriage.
This doesn’t imply that you may’t compensate for the added mass in your firmware and slice settings, however relying in your machine, it will possibly positively be the limiting consider your print high quality and print pace.
Bowden Extruder Strengths
All the advantages of a bowden are associated to not having the added mass of the extruder physique (motor, loafer, gear, and so forth) driving on the new finish carriage. With all different issues being equal, a printer with a bowden extruder is ready to transfer and print sooner, extra precisely, and extra exactly than the identical printer with a direct extruder.
Bowden Extruder Weaknesses
Essentially the most generally heard weak spot of bowden extruders is expounded to retraction and stringing or oozing. The elevated distance between the loafer/gear pinch level and the new finish will increase the hysteresis (lag) of the system. Most, if not all, of this may be adjusted for in slice settings and/or firmware changes, however we’ll depend it as a weak spot for the sake of this text.
Bowden extruders have extra friction on the filament as a result of it has to journey a lot farther from the loafer/gear pinch level to the new finish. This could necessitate the usage of a geared extruder for additional torque. The elevated friction may also make printing versatile filaments tougher.
That stated, this looks as if an acceptable time to handle the versatile filament matter.
Versatile Filaments
You’ll typically see or hear that you may’t print flexibles with bowden extruders. That is plainly unfaithful. It’s additionally not true that direct extruders can print with flexibles just because they’re direct. Whereas direct extruders can extra simply print flexibles for the explanations defined above, there’s actually only one factor essential to efficiently print versatile filaments on both sort of extruder – a totally constrained path from the loafer/gear pinch level to the new finish.
This illustration exhibits an unconstrained extruder and the problem that versatile filaments have in them.
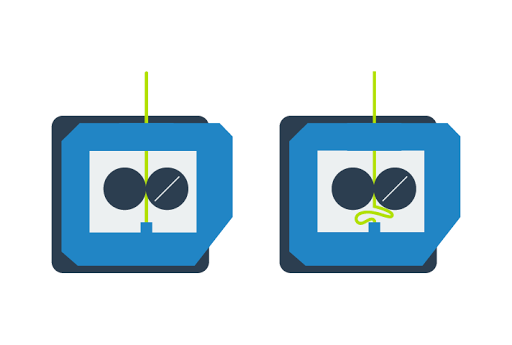
Typical extrusion habits with inflexible materials (left) vs versatile materials (proper)
That is true for each direct and bowden varieties. If there’s any room for the filament to go, it’s going to finally accomplish that, bind up, jam and trigger a failed print.
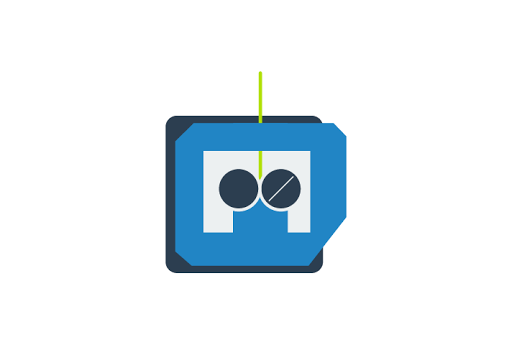
Absolutely constrained extruder gives acceptable
steering for versatile filaments
This picture exhibits a totally constrained extruder that may have the ability to efficiently print versatile filaments.
There’s nowhere for filament to go as soon as it passes by the loafer/gear pinch level.
It is a disassembled BondtechQR extruder. It’s a geared extruder that may be configured both as a direct or bowden, and has a totally constrained filament path. It’s out there for 1.75mm and 3mm filaments. Discover the “wedge” that extends as much as the pinch level on each the out and in feeds within the filament path. It’s a wonderful extruder, able to extruding any filament at present out there.
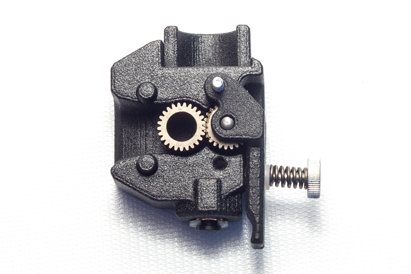
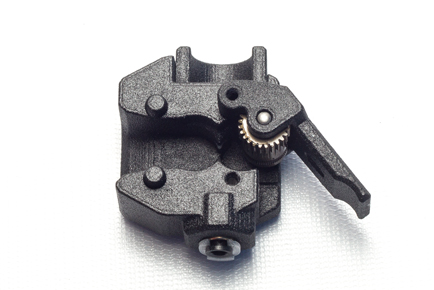
See the ‘wedge’ on the BondtechQR extruder, this gives help to the filament when extruding and is nice for versatile materials.
So which one is greatest?
That actually will depend on just a few issues aside from the extruder. What sort of printer do you may have? Cartesian or Delta? Do you intend to print quite a lot of versatile supplies? Do you wish to print as quick as doable whereas nonetheless sustaining accuracy?
Deltas don’t do nicely with added mass on the effector, so they’re higher suited with bowdens. In case your Cartesian machine isn’t very inflexible, you’d probably be nicely served with a bowden. When you’ve got a extremely inflexible, well-tuned cartesian, and pace isn’t tremendous vital, you’d probably get nice outcomes with a direct.
Regardless of the case, direct and bowden extruders are each going to be round for whereas, and neither is inherently higher than the opposite. We hope this text helped eradicate confusion and supplied sufficient info so that you can resolve which is the higher possibility to your particular printer and necessities.
Comfortable Printing!
[ad_2]
