



[ad_1]
Most metallic powders for additive manufacturing (AM) are produced by both gasoline or plasma atomisation strategies. Plasma atomisation processes are dearer however produce particles of extremely common morphology, particles with a smoothness and sphericity that sometimes surpass ranges achievable with gasoline atomisation.
This raises the query – do I would like a plasma atomised powder? Will superior morphology ship tangible profit that justifies paying a premium or can an appropriate gasoline atomised powder be equally match for function?
On the subject of powder manufacture, gasoline atomised powders can exhibit appreciable variability with respect to morphology, relying on the method specifics and the diploma of optimisation. Due to this fact, producers additionally must quantify the worth of superior particle morphology, to grasp what’s attainable when it comes to product differentiation. With acceptable optimisation, how successfully can gasoline atomised merchandise compete with plasma atomised alternate options?
Variations in morphology are straightforward to see and quantify, utilizing methods comparable to scanning electron microscopy and picture evaluation, however the outcomes don’t immediately elucidate in-process efficiency. Measuring bulk powder properties comparable to powder flowability brings complementary perception, serving to to quantify the influence of morphology in a course of related means, as these instance research show.
Figuring out another provide for laser metallic deposition
Markusson1 (Lulea College of Know-how, Lulea, Sweden) in a research carried out in collaboration with GKN Aerospace Engine Techniques (Trollhattan, Sweden) made an in depth bodily evaluation of 5 business Inconel® 718 powders; print trials had been additionally carried out. A major intention was to find out whether or not certainly one of 4 choices is likely to be an appropriate various to a powder already in use by GKN for laser soften deposition (LMD) functions.
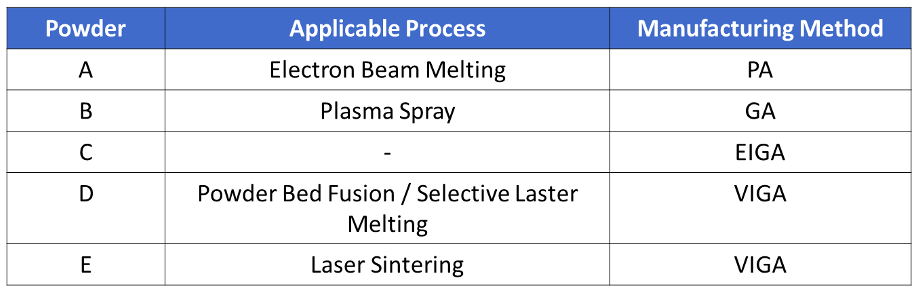
Desk 1: Particulars of the 5 business Inconel® 718 powders assessed for LMD
Desk 1 exhibits manufacturing route and designated software for the 5 powders. Powder C, the reference, is made by electrode induction gasoline atomisation (EIGA), whereas Powders D and E, are made in vacuum inert gasoline induction processes (VIGA). Each EIGA and VIGA supply tighter management of interstitial components and/or decrease danger of contamination, relative to different types of gasoline atomisation (GA – Powder B) and are widespread for top efficiency powders. Powder A, the fifth powder, is plasma atomised (PA).
The print trials recognized Powder A as the most effective various to Powder C. We will due to this fact use these knowledge to think about a distinct query to the one posed within the research. If Powder A, the plasma atomised powder, had been the reference, fairly than Powder C, then may Powder C have been differentiated from the opposite gasoline atomised powders by the testing carried out?
GKN had a specification in place previous to this work that included composition, manufacturing technique, Corridor Circulation Index, and particle dimension. All 5 powders met this specification. That’s to not say they had been similar, simply that any variations had been insufficiently vital to take powders outdoors of the established specification, limiting its worth for differentiation.


Determine 1/Desk 2: Powder morphology and particle dimension knowledge fail to securely determine the most effective various to Powder A.
Determine 1/Desk 2 exhibits powder morphology rankings and particle dimension distribution knowledge for the samples. Powder morphology rankings are derived from SEM photographs taking account of sphericity and satellite tv for pc content material; particle dimension was measured by laser diffraction. These knowledge don’t securely determine Powder C as just like Powder A. Variations in particle dimension are marked and whereas morphology rankings level to C, D and E are shut behind.
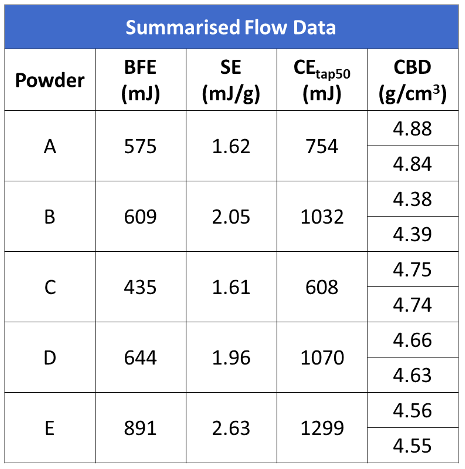
Desk 3: Dynamic movement properties and bulk density all level to Powder C as being most just like Powder A.
Tables 3 exhibits a choice of dynamic movement properties for the powders together with bulk density knowledge all measured utilizing the FT4 Powder Rheometer® (Freeman Know-how, Tewkesbury, UK). Dynamic movement properties level constantly to Powder C being a possible various to Powder A. They point out that Powders A and C are prone to carry out considerably comparably beneath most situations, suggesting that Powder C may very well be extra free-flowing. Conditioned bulk density values present additional reinforcement of the comparability.
Apparently, there are fewer variations between Powder A and Powder C, PA and GA respectively, than between the GA samples illustrating the vary of efficiency doable with GA supplies. These knowledge would simply justify a trial with Powder C, the outcomes of which might verify suitability.
These outcomes show the worth of dynamic powder properties and conditioned bulk density knowledge in quantifying the influence of morphological variations and differentiating provides in a related means. Particle pore knowledge additionally proved related to powder efficiency, notably with respect to print high quality.
Differentiating and optimising gasoline atomised powders
The previous research highlights the scope for variability between GA metallic powder provides, and by extension the chance to optimise gasoline atomisation to enhance efficiency. A second research by Chu et al2 gives additional proof of the worth of dynamic powder testing to assist such work. These researchers obtained two batches of AlSi10Mg powders, produced beneath totally different gasoline atomisation situations, and investigated their efficiency in laser powder mattress fusion (LPBF) printing. Batch 1, was produced utilizing a soften superheat of 180oC together with an atomising gasoline strain of 1.8 * 106 Pa whereas Batch 2 was produced at a decrease soften superheat, 110oC, and better atomising strain, 3.5 * 106 Pa.
This marked distinction in manufacturing situations had a significant influence on particle morphology. SEM photographs revealed Batch 2 to be far much less common than Batch 1 with extra proof of non-spherical particles, agglomeration, and satellites. As within the previous research measurements with the FT4 Powder Rheometer® quantified the influence of those variations whereas conventional powder testing strategies didn’t. Two conventional powder movement assessments had been utilized – angle of repose and Corridor Circulation Index. Repose Angle (RA) supplied no strong differentiation between the batches whereas Corridor Circulation Index testing gave a ‘no movement’ end in each circumstances. The powders had been insufficiently free-flowing to move via the funnel and no outcomes had been generated.
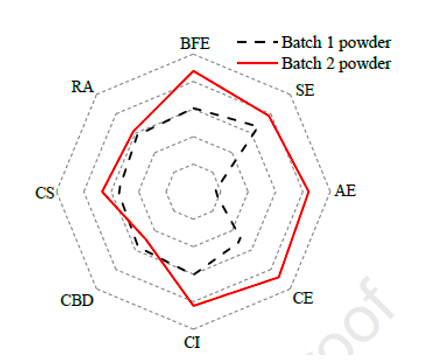
Determine 2: A radar plot of dynamic, shear and bulk properties identifies Batch 1 as superior; decrease values of all properties, besides CBD, are preferable. RA gives minimal differentiation.
In distinction, dynamic, shear and bulk density measurements determine Batch 1 as superior for print functions (see determine 2). It reveals higher flowability beneath a spread of situations (Primary Flowability Power (BFE), Particular Power (SE), Aerated Power (AE) and Consolidated Power (CE)) has decrease Cohesion (CS), decrease compressibility (Compressibility Index – CI) and better Conditioned Bulk Density (CBD). These knowledge counsel that Batch 1 will movement extra simply inside the printer and produce a extra effectively packed layer, a prerequisite for higher print high quality. Print trials verify the prevalence of Batch 1 with printed samples exhibiting increased high quality/fewer defects. These outcomes once more present how acceptable bulk powder testing is ready to translate morphological properties into quantifiable positive aspects in course of related parameters.
In conclusion
Steel powder producers know how one can enhance particle morphology, how one can ship smoother, extra spherical particles that may improve print high quality, however such enhancements come at a value. This makes it very important to grasp the worth of any positive aspects. By assessing SEM micrographs it’s straightforward to see an enchancment in particle morphology however to not consider its significance. That is the place bulk powder testing has an vital position to play. By measuring the appropriate properties – notably dynamic movement properties – it’s doable to find out whether or not an enchancment in morphology will truly make a distinction to printing efficiency. Bulk powder testing permits you to quantify what you want and determine the availability that meets these wants in probably the most cost-efficient means, nonetheless it’s made.
With due to Lisa Markusson, former Masters Scholar at Lulea College of Know-how in Sweden, and Lars Östergren, Design Engineer Idea Improvement Additive Manufacturing for GKN Aerospace Sweden AB.
1L. Markusson ‘Powder Characterization for Additive Manufacturing Processes’ Thesis report. Revealed 2017
2F. Chu et al ‘Affect of satellite tv for pc and agglomeration of powder on the processability of AlSi10Mg Powder in Laser Powder Mattress Fusion’ J of Mat Res and Tech https://doi.org/10.1016/j.jmrt.2021.02.015
Subscribe to Our Electronic mail E-newsletter
Keep up-to-date on all the newest information from the 3D printing business and recieve info and provides from thrid occasion distributors.
[ad_2]

