



[ad_1]
Most customers of Fused Filament Fabrication (FFF) 3D printing know-how perceive that the decision on completed prints / elements is often 100 microns or better with some producers claiming printer decision of fifty microns.
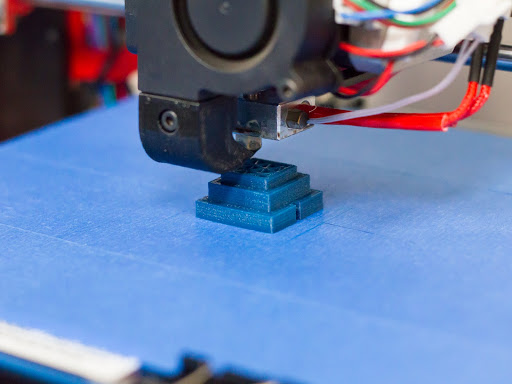
Determine 1: Printing the Dimension Accuracy Mannequin
Decision is just one standards that skilled customers apply to find out the standard and worth of a 3D printer. In an annual competitors, Make Journal convenes a Digital Fabrication Shootout to evaluate the standard of machines at completely different worth factors. Make’s testing standards is beneficial for any proprietor or person of a 3D printer to find out the tolerances and high quality of their tools.
The standards and corresponding Take a look at Print Fashions run the gamut from precision / accuracy and end to machine capabilities. There are 9 main components to contemplate through the testing of your 3D printer. These components are listed under and expanded upon with causal particulars and strategies of mitigation with the intention to produce the very best high quality fashions and elements.
Dimensional Accuracy
Dimensional accuracy is nothing greater than demonstrating that your completed print / half possesses the identical dimensions of the unique half or design. That is usually problematic when the bottom or backside of an element is subsequent to the mattress. Warmth and curing might trigger warping and infrequently the preliminary base layer of a print is programmed with extrusion charges in extra of 100% to make sure that the half adheres to the mattress (See Figures 1 and a pair of). This leads to a wider preliminary layer and with ensuing dimensions better than designed. Many customers try to mitigate this concern by using a raft base earlier than printing the primary layer of the particular half.
One must also think about the implications of infill on the finished half. With 100% infill, the quantity of fabric when cured might overlap or prolong the completed half past the specified dimensions. There may be additionally a chance for warping through the curing course of. From expertise, a MatterControl infill setting at 85% works greatest for a top quality most infill.
Lastly, remember that the layer peak set for the z-axis has a direct correlation to dimensional accuracy within the z-direction. Typically occasions, the very best methodology to make sure dimensional accuracy is to print at a layer peak of 100 microns and to set the perimeter speeds between 15 – 30 mm/s.
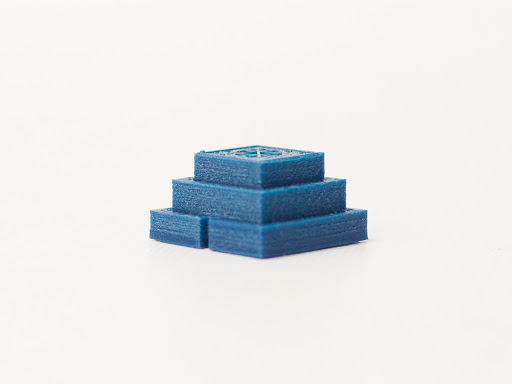
Determine 2: Instance of Over Extrusion and Warping
Horizontal Floor End
Subsequent to warping and stringing, floor end is the attribute most observed by the top person. Floor end is usually materials particular with PLA having a notoriously poor floor end. One methodology to enhance the horizontal floor end is to decrease the highest / backside layer extrusion speeds to inside 15 – 30 mm/s. It might additionally assist to extend the depend of high / backside layers to 5 to make sure a clean end (See Determine 3). Publish processing could be an efficient instrument to bettering floor finishes. Supplies similar to ABS are simply sanded and sealed and a shiny end could also be produced by means of an Acetone Vapor Smoothing course of. Simply keep in mind that most 3D printed elements as a part of an finish product are usually submit processed.
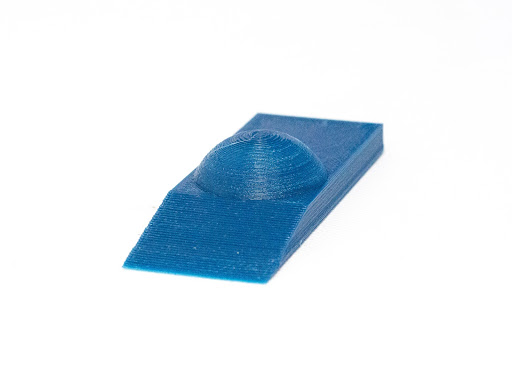
Determine 3: Discover the Roughness of the End As a result of Layer Top Floor Angle
Vertical Floor End
High quality vertical floor finishes are a direct results of layer peak, nozzle diameter and perimeter extrusion speeds. Growing the variety of perimeter layers would most likely not have an effect on the floor end within the z-direction, however printer extrusion velocity and layer peak must be adjusted for the very best end. Additionally, bear in mind the kind of supply materials that you’re utilizing when adjusting the extrusion velocity and maintain your layer heights between 100 – 200 microns. As at all times, submit processing will improve the floor end of a top quality half or finish product (See Figures 4 – 6).
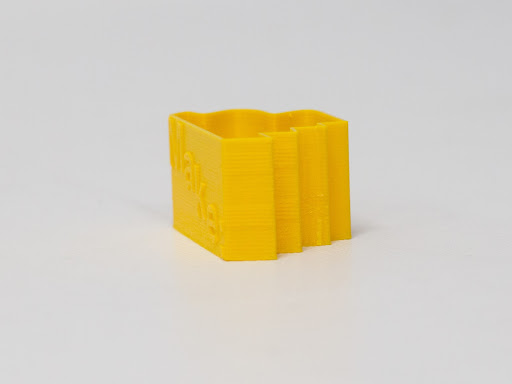
Determine 4: Discover That the End on Sharp Angles is Not as Clean as on Curves
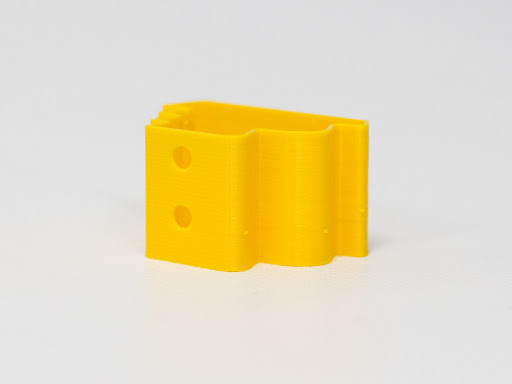
Determine 5: Curved Surfaces are Often Smoother
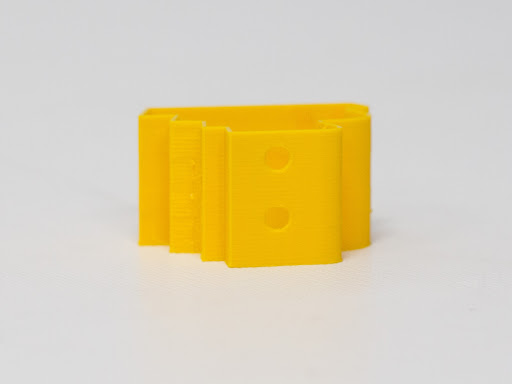
Determine 6: Angled and Curved Surfaces
Overhangs
Overhangs are the bane of designers and engineers when creating fashions for 3D printing. The prevailing steering is both to place the half so there are not any overhangs or to offer precise or 3D printed helps within the z-direction as soon as printing begins. When 3D printing with overhangs, the very best steering to recollect the 45 diploma rule. Most printers can print overhangs as much as 45 levels with little points, however angles as much as 70 levels could also be achieved when you have your 3D printer dialed in (See Determine 7). Moreover a layer peak discount and a decrease extrusion velocity might help in printing angles better than 45 levels. One other methodology of mitigating the overhang difficulty is to design in chamfers or fillets on the stable mannequin. This can help the printer in adjusting for the overhang hole. In the long run, trial and error whereas adjusting layer peak and extrusion velocity will reveal the utmost overhang angle that your printer will have the ability to efficiently mitigate.
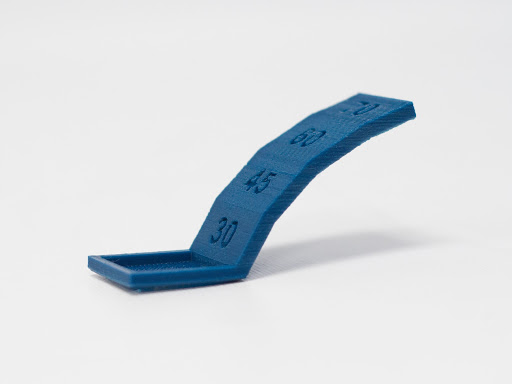
Determine 7: Discover the Roughness of the End at 60-Plus Diploma Angles
Retraction Efficiency
Stringing is a visual and submit processing nightmare. It’s most frequently obvious when making an attempt to print a couple of mannequin or half concurrently or when a mannequin or half has giant gaps or unfavorable house. Stringing is a direct results of the retraction size and velocity settings for a selected print (See Determine 8). Nevertheless, don’t be dismayed. A useful reference information on retraction and learn how to mitigate stringing could also be discovered at Retraction: Simply say “No” to Oozing.
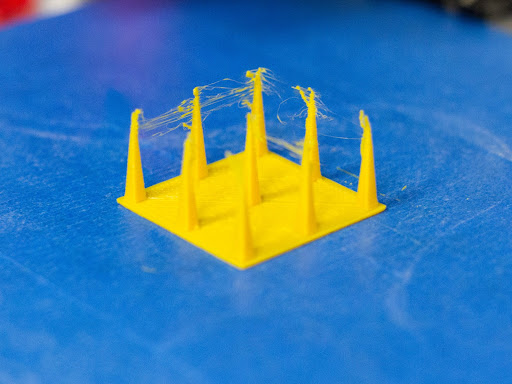
Determine 8: Instance of Stringing As a result of Retraction
Bridging
Bridges are printed flat sections that cross open spans within the mannequin. Printing bridges is one thing of an “artwork” and plenty of lovers make movies of distances that they have been in a position to span on their printers in a typical “are you able to beat that” bravado. With most bridges whereas printing at common speeds, a span of 50mm is widespread. Nevertheless, some printers can do even longer spans and the size of the span might also be depending on the kind of materials used. When bridging, maintain the extruder velocity between 20 – 30 mm/s. The default setting for bridges in MatterControl is 20 mm/s (See Determine 9). Simply keep in mind that the quicker the velocity, the better the possibilities are for filament sags. Trial and error is the modus operandi for this course of as you slowly synch your machine with the optimum supplies and speeds.
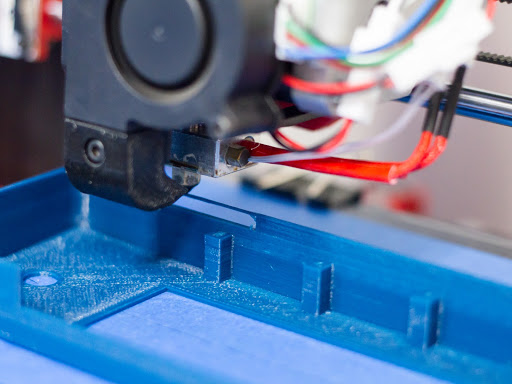
Determine 9: Instance of Bridging
Adverse House Tolerance
One other thorn within the sides of designers and engineers is the unfavorable house tolerance difficulty. This actually comes into play when making an attempt to hitch prints or elements collectively into one meeting. Adverse house dimensions are materials particular and are affected by curing and floor end. Many of those points could also be mitigated by means of design, however trial and error together with your particular machine will normally give you a transparent path ahead (See Figures 10 and 11). For extra info on this topic, be happy to confer with the reference article MatterHackers Lab: Design 3D Printed Assemblies.
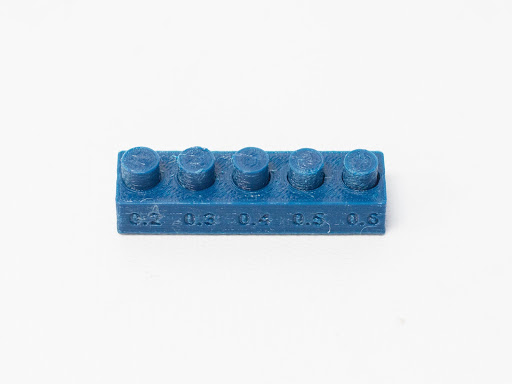
Determine 10: Adverse House Take a look at Mannequin With a Adverse House of .2 and .3mm
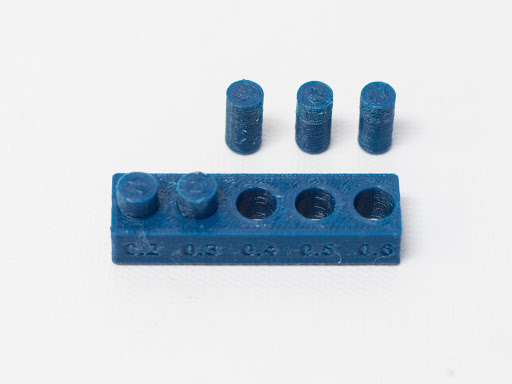
Determine 11: Discover That the Two Pins Printed Had been Not Capable of be Eliminated
Z-Wobble
Z-wobble is fully a mechanical difficulty and is almost certainly brought on by out-of-tolerance mechanical elements and / or improper machine calibration (See Determine 12). It’s prevalent with Cartesian sort printers, particularly these with twin z-axis ball screws. Cantilever stiffness additionally performs into the wobble phenomena as usually Cartesian printers have a whole lot of “play” within the printer carriage itself. As a way to mitigate this difficulty, ensure that your extruder and printer carriage are moderately stiff and that the carriage traverses alongside the cantilever in a degree method. In different phrases, ensure that your machine is degree and calibrated appropriately. Some elements over time will put on, so ensure that the screws / ball screws and bearings are maintained, lubricated and in good situation. If there was some put on, you might wish to change the elements. In the event you hear any grinding or sounds of friction, be sure you revisit element and mattress leveling processes. The reference article The best way to Calibrate Your Extruder will lead you thru the calibration course of for extrusion.
The appearance of Delta printers solves or at the very least mitigates the z-wobble difficulty. Z-wobble is virtually eradicated on a Delta printer because of much less weight on the extruder housing and in the usage of three towers from which to droop the extruder. Most Delta printers make the most of the Bowden answer which retains the extruder motor off of the carriage. This elegant answer has improved upon lots of the points related to a regular Cartesian printer.

Determine 12: Instance of Z-Wobble (Picture courtesy of Danie Grobbelaar)
Help Materials
In case you have been 3D printing for various years, you’ll know and perceive the challenges of including and using assist materials. Older slicing options have been infamous for printing assist materials that was nearly not possible to take away, with some helps really adhering and melting to the half itself. Immediately’s controllers present a assist answer that’s a lot simpler to take away and infrequently locations “air gaps” between the precise half and the supplies forming the helps. For a base setting in MatterControl, make the most of the ten% infill setting of line patterns at 2.5mm intervals in producing helps. Additionally, embody a raft (the article Printing with a Raft supplies background info) with the helps to make sure that the assist materials adheres to the print mattress. An “air hole” of .3mm is the default, however you might wish to alter this setting on an as wanted foundation. Be happy to extend the infill settings and reduce the intervals do you have to want extra assist all through the mannequin. The objective of helps is to offer sufficient materials so that each one sides of the mannequin could also be printed coupled with ease of elimination of the assist materials as soon as the print is completed. For these with twin extruder printers, you might wish to make the most of assist filament to incorporate HIPS and / or PVA in one of many two extruders whereas printing.
In abstract, the standard of your 3D printed elements hinges simply as a lot on understanding your machine’s tolerances and capabilities because it does on print mattress leveling, machine element leveling, machine calibration and the design and positioning of the mannequin / half for printing. Printing the Take a look at Print Fashions in your machine with completely different supplies and settings will make sure that you understand your machine’s capabilities and the place your tolerances could also be adjusted. This like all good issues in life will take time, so step again and benefit from the journey. You’re a grasp creator and your expertise and capabilities will produce distinctive elements and merchandise for all to take pleasure in.
[ad_2]
