



[ad_1]
For most individuals, ASA filament is comparatively extraordinary throughout the 3D printing group. Whereas is is probably not too widespread, it’s a wonderful materials when you might want to 3D print one thing that’s meant for outside use, like a planter, backyard gnome, or for any random outside fixture. ASA is similar to ABS filament, and prints about the identical too, however what it holds over ABS is that white ASA takes quite a bit longer to begin yellowing within the solar or to begin deteriorating and shedding its energy. Should you’ve by no means printed with ABS or ASA earlier than, there’s a pair ideas and methods you wish to know earlier than you get began, and with this information, you’ll be printing with ASA 3d printing filament very quickly.
Step 1: Be certain your first layer is correct
Making your first layer proper is a two-part course of: you might want to ensure that your mattress is degree, and you might want to ensure that the nozzle is the appropriate distance from the mattress.
Leveling the Mattress
To degree the mattress, you might want to comply with the directions supplied along with your printer. Each printer has it’s personal methodology, with some having guided wizards, auto mattress leveling, otherwise you’re fully by yourself. Usually, 3D printer mattress surfaces are leveled utilizing three or 4 screws attaching the mattress to a carriage. Tightening or loosening these screws modifications the aircraft the mattress is on, in case your mattress itself isn’t bent. On the whole, although, the process to degree a mattress is:
- Transfer your print head out of the best way of the mattress to forestall it from crashing if it’s too shut.
- Dwelling the Z axis. It will transfer the nozzle to as near the mattress it could get. If there’s room between the nozzle and the mattress, excellent. If there isn’t room, tighten the screws below the mattress till there’s about 1mm of area.
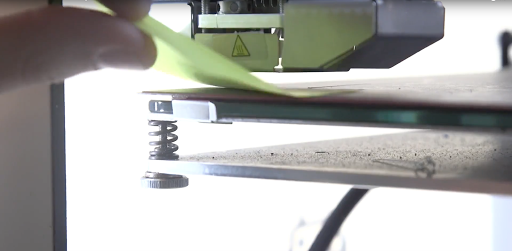
- Transfer the print head above one of many three or 4 screws and insert a bit of paper between the mattress and the nozzle.
- Gently loosen the screw till there’s a very slight quantity of resistance between the mattress and the nozzle. Simply sufficient to note, however not sufficient to require pressure to maneuver the paper out.
- Repeat this with the remainder of the screws. The hot button is to get the identical resistance in any respect factors; this implies your mattress is degree.
Adjusting Nozzle Distance
Now that the mattress is degree, you might want to ensure that the nozzle is on the proper distance from the mattress.
- Be certain your mattress materials of alternative is utilized at this level.
- Begin a print with a skirt that covers your complete space of the mattress.
- Watch how the filament is laid down. Is it actually smearing out the edges of every cross and appears prefer it’s effervescent up towards one another? You’re a lot too low, and will bump it up a bit of bit at a time. Is there a transparent distinction between every cross of the skirt? You’re too far-off and have to decrease the nozzle.
- You may both flip every screw the identical quantity and regularly take a look at till the skirt comes out okay or you’ll be able to change the Z Offset in MatterControl and typing in your required change. Maintain it to 0.02mm at a time till you discover the appropriate distance.
Step 2: Print mattress and adhesion.
Should you don’t have a heated mattress, ASA isn’t going to be just right for you. Identical to its predecessor ABS, ASA is de facto temperature delicate and warps and splits in case your temperatures aren’t fairly proper.
Should you do have a heated mattress, right here’s what you are able to do:
- Print with a brim. I exploit a brim of about 15 loops. I very hardly ever want extra loops than that, however with the appropriate temperatures, an enclosure, and adhesive, typically I can get away with not utilizing a brim in any respect.
- A light-weight spray of Aqua Web Hairspray on the mattress and printing with a mattress temperature of 110C works very well. 110C works in case your printer could make it there, however for some 3D printers, they simply can’t make it. In that case, print at no matter it’s max temperature is and hope for one of the best. I’ve been profitable as little as 90C earlier than, however that was a really effectively calibrated machine. As well as, ensure you’re utilizing particularly Aqua Web, although; different manufacturers may match however Aqua Web is tried and true.
- If you need one thing extra managed than hairspray, it’s also possible to make ABS juice as described in our video and article (right here) to brush on a mattress adhesive as an alternative of a positive mist on the within of your printer.
- You may also use Kapton tape on prime of your heated mattress along with hairspray. It helps uniformly unfold the warmth in your mattress so that you don’t have warpy corners, and it produces some very nice, shiny bottomed prints.

Step 3: Calibrating your print temperature.
- For ASA, I usually print at 250 levels Celsius and a mattress temperature of 110 levels Celsius.
- Chances are you’ll have to positive tune your printer to get outcomes you might be pleased with, and you are able to do that by adjusting temperatures up or down 5 levels at a time.
- Printing too sizzling for ASA isn’t as huge of an issue as printing too chilly:
- A chilly ASA print will warp or cut up, or have horrible layer adhesion,
- A sizzling print can have higher layer adhesion, with some stringing and a few rougher overhangs.
Step 4: Tricks to Remedy Warping and Splitting
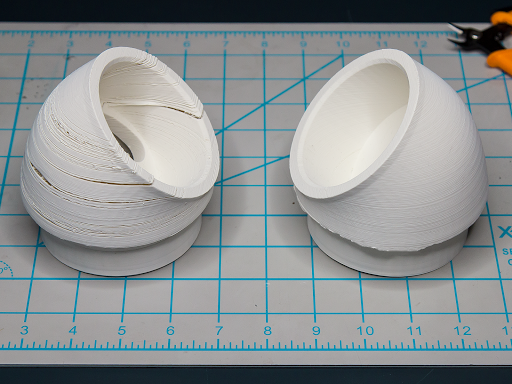
Even in the event you’ve completed all that proper, you would possibly nonetheless have some points along with your prints and that’s the identical issue that ABS faces: it warps. A slight draft and you’ve got a ruined print from both the corners warping up or a cut up forming on that layer – the place the earlier layer cooled faster than the following layer may adhere to it. Right here’s two key issues to care for it:
- Construct an enclosure on your printer, both as fundamental as a trash bag, some plastic sheeting and PVC like in our different (video), or construct one out of LACK tables from IKEA, no matter works. The essential thought is maintain warmth in and drafty cool air out.
- Flip off layer cooling followers. These can cool your prints too shortly, which works effectively for PLA and even PETG, however for ASA, it’ll trigger splits and points in your print. You might be able to flip them as much as a delicate 10% with some success, however do a pair small take a look at prints earlier than committing to a 24 hour ASA print with the followers on.
Step 5: How To Change Filament
- One of many earliest errors I made after I received into 3D printing was not understanding methods to change filament.
- One of the best process is to comply with the directions supplied along with your printer as some have automated filament altering routines.
- For any others, warmth up your nozzle to your printing temperature.
- At about 120, gently pull on the filament whereas releasing pressure from the extruder (by both pushing on the lever of the loafer or releasing the loafer altogether).
- As soon as the filament reaches a sizzling sufficient temperature (close to its glass transition), it’s best to be capable to pull out the entire ASA, even what was already within the nozzle, lowering coloration mixing whenever you add the following filament.
- After you have eliminated the filament, push the brand new filament in till you see filament of the identical pure coloration popping out of the nozzle.

Step 6: Common Upkeep and Care
Another fast ideas that ought to show useful:
- Commonly clear the extruder gear and verify the stress. Because the drive gear presses down on the filament, it chews it just a bit bit with a view to transfer it. Progressively the tooth of the gear fills and it received’t be capable to extrude or it’ll underextrude. A toothbrush or a small wire brush could make fast work of this filament mud. Some extruders have adjustable tensioners, and you may tune that too to get extrusion to work and never chunk into the filament too laborious.
- Should you aren’t in a position to extrude ASA in any respect and your hotend is at temperature, your nozzle is likely to be clogged. Try our video on methods to unclog a nozzle to assist stroll you thru the steps of clearing it.
And that’s it! It’s plenty of info to course of, however altogether it’s best to have sufficient to work from to get began printing ASA and printing it efficiently.

[ad_2]
