



[ad_1]
There are a number of totally different PLA composite supplies on the market, lots of which use steel. Filaments like Steelfill, CopperFill, or Magnetic Iron PLA are actually cool to print with and might create some superb ornate prints, however there are some steps you will must take first earlier than taking the plunge and printing with metal-infused PLA.
Notice!
Steel-infused PLA doesn’t make the filament tackle the fabric properties of the steel it’s infused with. Do not count on to take your stainless steel-PLA carabiner and use that to go mountaineering. These filaments are purely for ornamental functions, and in reality the powdered steel within the plastic really makes it extra brittle than the plastic alone.
Step 1: Use the Proper Nozzle
Most 3D printers include a brass nozzle, which is nice for thermal conductivity and having simple and fast extrusion. However brass is smooth for a steel, and any type of steel primarily based PLA goes to put on down your brass nozzle. The tougher steel throughout the PLA will scrape away on the nozzle orifice, taking your pristine 0.4mm nozzle probably as much as a 0.5mm nozzle by the tip of the roll. There are nevertheless, abrasive resistant nozzles you’ll be able to often swap into your printer, like chrome steel, hardened metal, or the Olsson Ruby.
- “Put on Resistant” nozzles, are often brass with a nickel plating, so whereas they’re designed to withstand any issues, once you begin printing with ColorFabb Steelfill, that plating goes to vanish.
- Stainless-steel nozzles are an excellent step up from brass, and can final you an honest period of time, however nonetheless aren’t the very best you’ll be able to put in your hotend.
- Hardened metal nozzles aren’t nearly as good as brass with regards to conducting warmth, however slightly hotter extruder temperature and it’ll make up for it, and the hardened metal is resistant sufficient to probably final years printing abrasive supplies.
- The Olsson Ruby is the end-all-be-all nozzle, designed to face up to nearly something you’ll be able to throw at it. Particularly designed to print boron-carbide filament, this nozzle will final nearly endlessly.
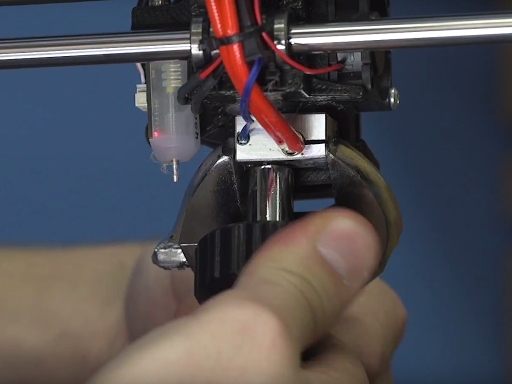
Altering your nozzle is absolutely easy and can develop your materials printing capabilities
Step 2: Be sure your first layer is true
Making your first layer proper is a two-part course of: you must be sure that your mattress is stage, and you must be sure that the nozzle is the appropriate distance from the mattress. Some printers now include auto-leveling options or particular leveling routines, so comply with the directions offered along with your printer.
Leveling the Mattress
Normally, 3D printer mattress surfaces are leveled utilizing three or 4 screws attaching the mattress to a carriage. Tightening or loosening these screws modifications the aircraft the mattress is on, in case your mattress itself isn’t bent. Usually, although, the process to stage a mattress is:
- Transfer your print head out of the best way of the mattress to forestall it from crashing if it’s too shut.
- Residence the Z axis. This may transfer the nozzle to as near the mattress it might get. If there’s room between the nozzle and the mattress, good. If there isn’t room, tighten the screws below the mattress till there’s about 1mm of area.
- Transfer the print head above one of many three or 4 screws and insert a chunk of paper between the mattress and the nozzle.
- Gently loosen the screw till there’s a very slight quantity of resistance between the mattress and the nozzle. Simply sufficient to note, however not sufficient to require pressure to maneuver the paper out.
- Repeat this with the remainder of the screws. The secret’s to get the identical resistance in any respect factors; this implies your mattress is stage.
Adjusting Nozzle Distance
Now that the mattress is stage, you must be sure that the nozzle is on the proper distance from the mattress.
- Be sure your mattress materials of alternative is utilized at this level.
- Begin a print with a skirt that covers the whole space of the mattress.
- Watch how the filament is laid down. Is it actually smearing out the perimeters of every move and appears prefer it’s effervescent up towards one another? You’re a lot too low, and will bump it up slightly bit at a time. Is there a transparent distinction between every move of the skirt? You’re too distant and must decrease the nozzle.
- You’ll be able to both flip every screw the identical quantity and frequently check till the skirt comes out okay or you’ll be able to change the Z Offset in MatterControl and typing in your required change. Maintain it to 0.02mm at a time till you discover the appropriate distance.
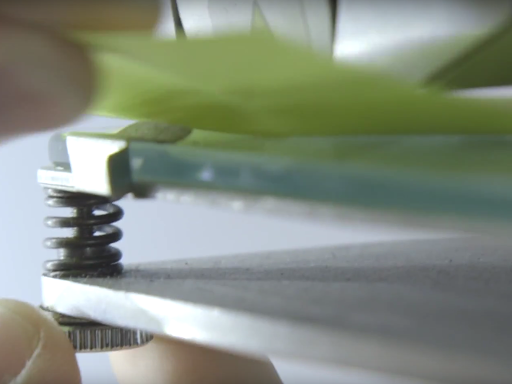
Understanding tips on how to stage your mattress is extremely useful.
Step 3: Print mattress and adhesion.
Identical to common PLA, all the identical adhesion methods apply. From kapton tape, to hairspray, to gluestick. No matter you employ once you’re printing common PLA will work simply positive right here. Watch out when printing on a floor like BuildTak or PEI, because the metal-infused PLA is a extra brittle than common PLA, and any type of wrenching on an element to separate it might break it.
Step 4: Calibrating your print temperature.
- For steel PLAs, I usually print at 215 levels Celsius and a mattress temperature of 60 levels Celsius.
- You could must positive tune your printer to get outcomes you might be proud of, and you are able to do that by adjusting temperatures up or down 5 levels at a time.
- Since these filaments are PLA primarily based, you must watch out of how excessive your printing temperature goes. Too excessive and also you danger ugly overhangs or drooping. Do some experimenting with small components to gauge what works greatest in your printer.
Step 5: Layer Cooling Followers
Identical to common PLA, layer cooling followers are a should. Too little cooling, and all of your overhangs and bridges could have some drooping. Whether or not it is a correct layer cooling fan mounted to your printhead or a desk fan to the aspect of your printer, you will want one thing operating. Print along with your cooling followers at 100% if in case you have them and also you’re good to go.
Step 6: How To Change Filament
Altering to a metal-PLA from some other is not any totally different than ordinary, simply warmth up your printer to the earlier printing temperature and extrude the metal-PLA by means of it. This could soften out the entire outdated filament, and maintain operating it till the brand new filament runs by means of. If you end up accomplished printing with metal-PLA, it is the identical process of heating it as much as whichever materials runs hotter (so in case your new materials is ABS, warmth it as much as ABS temperature), after which extrude the brand new materials.
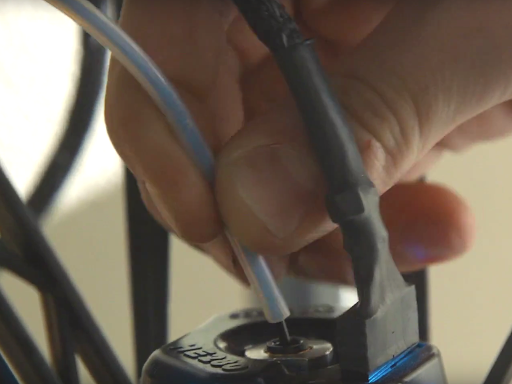
Altering filament the appropriate means will prevent a number of headache diagnosing clogs.
Step 7: Print Speeds
The print pace for steel PLAs are akin to common PLA, or just a bit slower. The powdered steel within the filament makes the filament extra brittle than common PLA, so any type of pressure or kinking to the uncooked filament will trigger the filament to interrupt. Ensure that the filament path from spool to extruder is nicely constrained, and by that I imply a straight path to the extruder, to lower the possibility of it breaking earlier than it may be extruded. In some circumstances, you could possibly print in any respect the identical speeds as common PLA.
Step 8: Common Upkeep and Care
Another fast suggestions that ought to show useful:
- Commonly clear the extruder gear and verify the strain. Because the drive gear presses down on the filament, it chews it just a bit bit with a purpose to transfer it. Regularly the tooth of the gear fills and it gained’t be capable of extrude or it’ll underextrude. A toothbrush or a small wire brush could make fast work of this filament mud. Some extruders have adjustable tensioners, and you may tune that too to get extrusion to work and never chew into the filament too exhausting.
- If you happen to aren’t capable of extrude ASA in any respect and your hotend is at temperature, your nozzle could be clogged. Take a look at our video on tips on how to unclog a nozzle to assist stroll you thru the steps of clearing it.
And that’s it! It’s a number of info to course of, however altogether you need to have sufficient to work from to get began printing steel infused PLA and printing it efficiently.
Step 9: Submit Processing
There are a pair other ways to go about post-processing steel PLA:
- Use a rock tumbler. Now this does not must be something costly, you’ll be able to simply get one on-line or an inexpensive one from a ironmongery store, but it surely’s basically a motor that rolls a small container along with your half inside it and a few abrasive materials. You will additionally want to purchase “media” which is the precise substance that’s abrasive to put on down and polish the 3D print. If you happen to select this methodology, be sure that your print would not have any small protrusions or these might break off, as a result of you’ll be leaving it within the tumbler for the higher a part of per week.
- If you happen to’re utilizing magnetic iron PLA, you’ll be able to rust it! That is as simple as scuffing you mannequin with some metal wool or a wire brush to open up extra floor space to just accept the answer you are about to make. In a container sufficiently big to suit your 3D print, combine water, salt, hydrogen peroxide, and vinegar in no particular ratio, and depart it in a single day, or at the very least a pair days.
- Very similar to different filaments, you’ll be able to sand and polish your 3D print. Begin off with a low 80 grit to essentially break down the layer traces, and progressively transfer as much as 1000 or 2000 grit earlier than utilizing some sharpening compound to essentially make it shine.
- A better and far less complicated methodology for a fast post-process is burnishing. Use some metal wool and the again of a clean piece of steel, like a spoon, to only polish the outer floor of the mannequin to make it shine. This would possibly not break down the layer traces, however it would at the very least make for a very fairly print.
Step 10: Help Settings
Watch out along with your help settings, and even think about using some small air hole assessments, as a result of help materials is a little more vulnerable to welding to your half. Since your print is way more brittle than common PLA, any torque or pressure utilized to the remainder of the mannequin in attempting to take away help might really break items off. Go simple in your 3D print, and do some testing earlier than committing to a 24 hour supported print.
And that’s it! It’s a number of info to course of, however altogether you need to have sufficient to work from to get began printing steel infused PLA and printing it efficiently.
Completely happy printing!
[ad_2]
